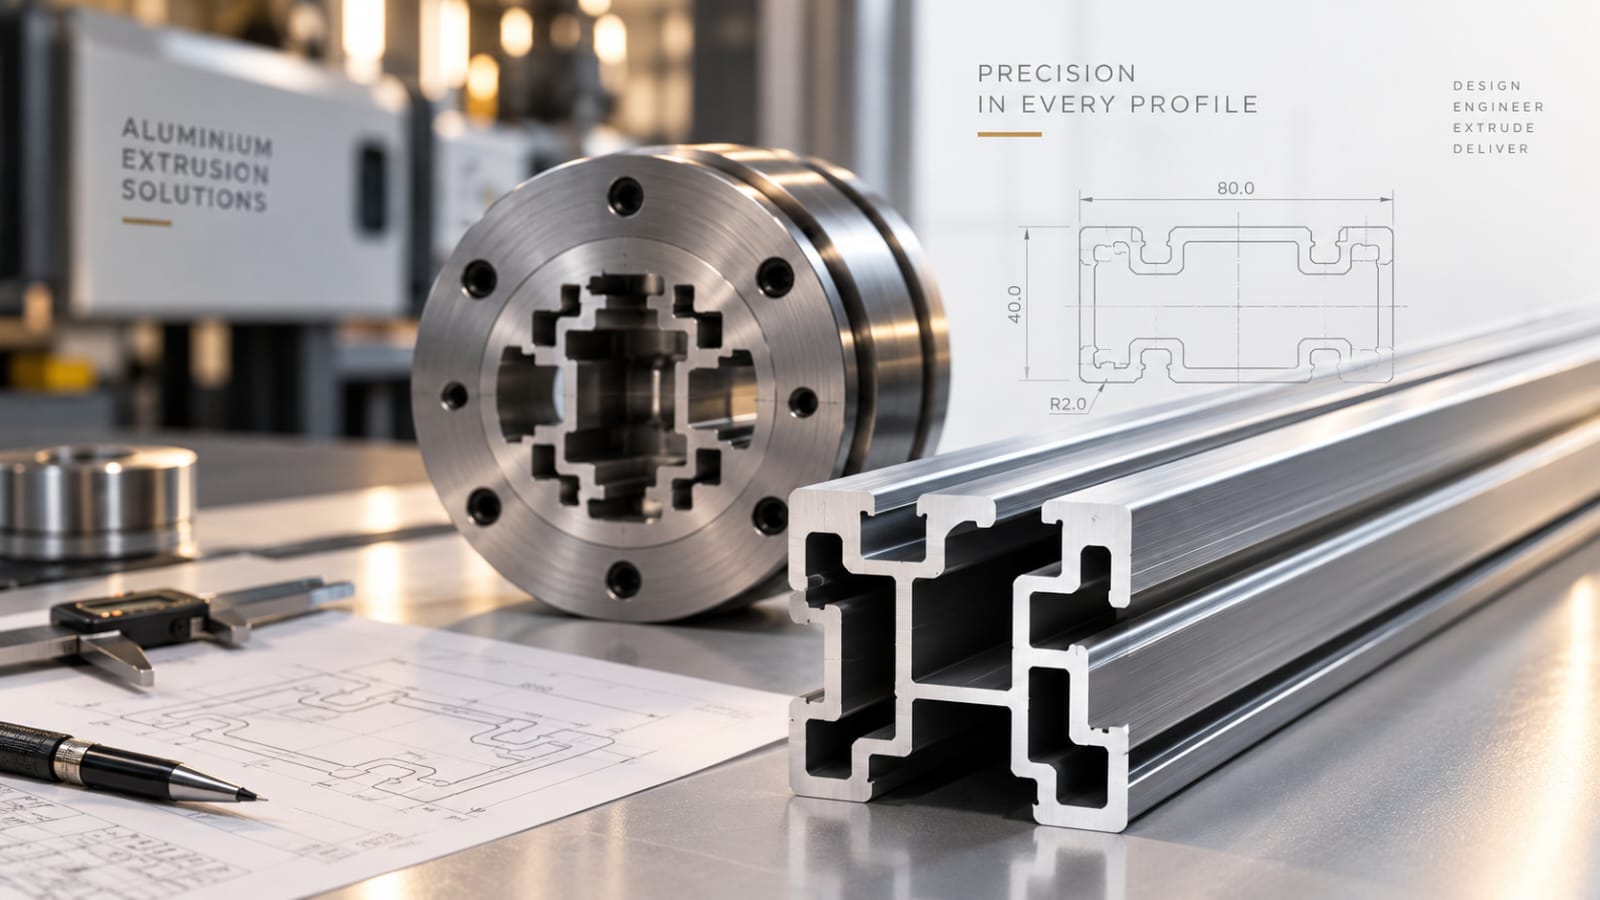
Aluminium Extrusion Dies & Die Rework

Precision
in every

die.

Die making for aluminium profile extrusion. Share your section drawing, alloy, press details and requirement; we will review the profile and advise the suitable die arrangement.

AMIT ENGINEERING / 01 Vadodara · Gujarat · India
Scroll to explore
About AMIT Engineering

Built for
precision.

We make new extrusion dies and rework running dies for aluminium profile manufacturers.

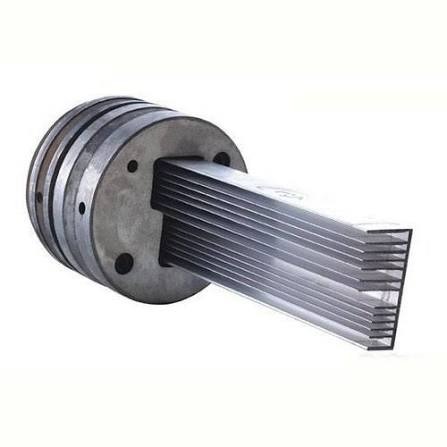
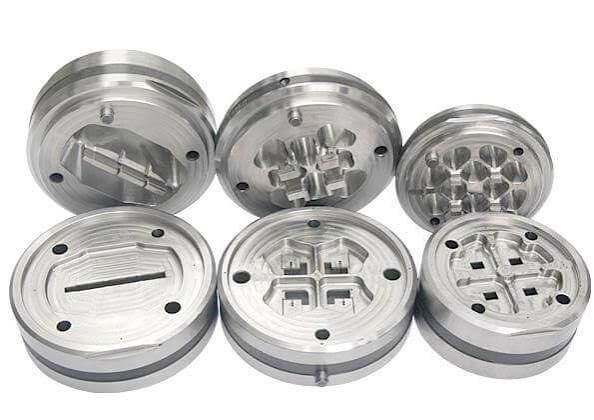
AMIT ENGINEERING works on the tooling that shapes aluminium profiles. Our scope includes solid dies, hollow/porthole dies, semi-hollow dies, die sets and corrective rework for production tooling.

A workable die starts with the actual profile: circumscribed circle, wall thickness, alloy, press container size and extrusion requirement. We use these inputs to determine die type, bearing approach and the required supporting tooling.

Email the workshop
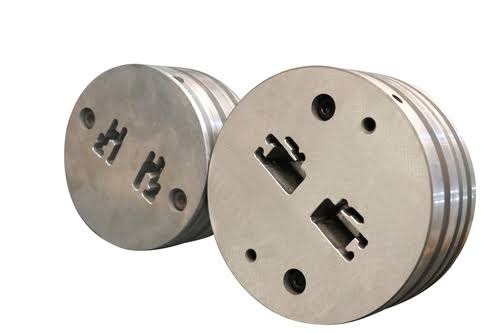
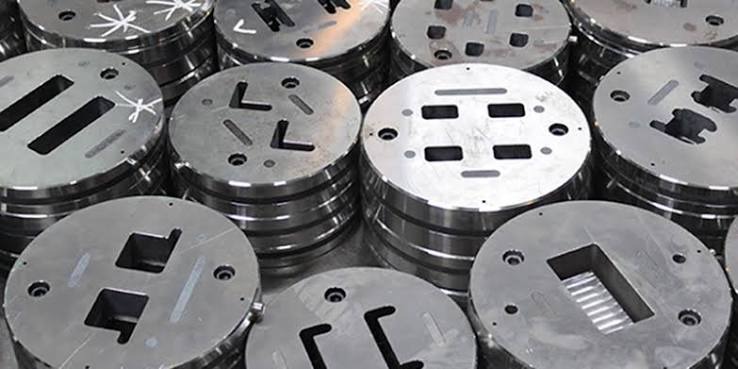
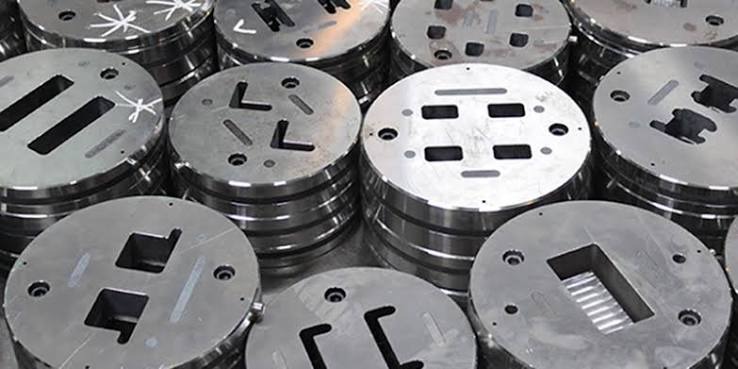
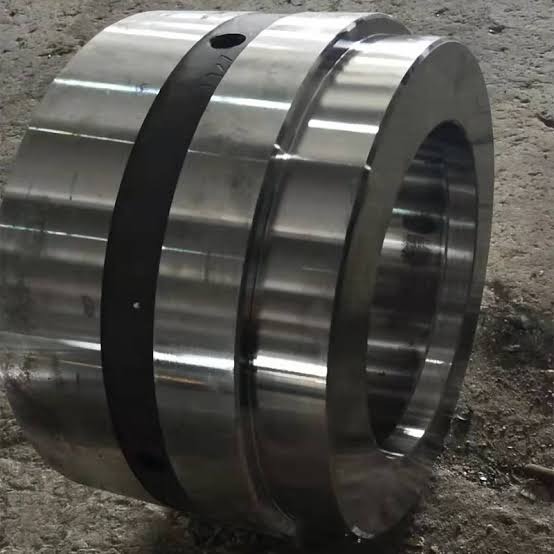
Polished circular industrial tooling component from AMIT ENGINEERING AE / DETAIL 01 Extrusion die — profile-specific tooling
01

Die Design & CNC

Profile review, die layout and machining planning based on the section drawing and extrusion requirement.

02

Solid, Hollow & Semi-Hollow

Tooling for open sections, enclosed hollow sections and profiles with critical tongues or narrow gaps.

03

Die Correction

Bearing adjustment and die correction based on profile output and feedback from the extrusion press.

04

Rework & Repair

Assessment, machining and correction work to help bring existing production tooling back into service.
What we make

Die types for
every profile.

The die type follows the profile geometry. We help identify the suitable approach before machining starts.

03

Semi-Hollow Dies

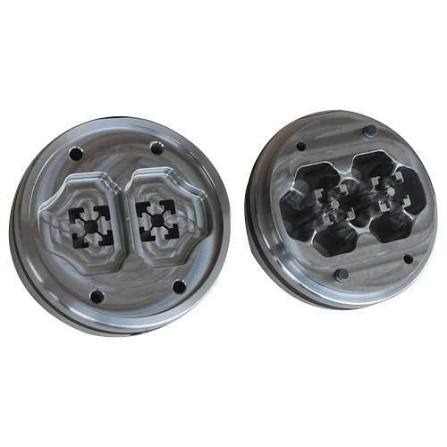
For profiles with a partially enclosed area, such as channels with a narrow opening. The die layout must protect critical tongues while controlling flow around the section.

04

Profile Dies

Die development for a customer-specific section drawing. We review profile geometry, circumscribed circle, wall thickness, alloy and press information before finalising the tooling approach.

05

Die Components & Tool Stack

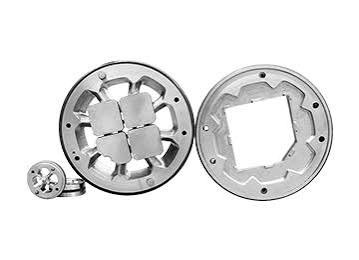
Supporting parts for the extrusion die assembly, including backers, bolsters, sub-bolsters, rings, caps and other profile-specific components as required.

06

Die Repair & Rework

Rework for production dies that need correction or restoration. Scope can include bearing correction, pocket modification, re-machining and other work after inspection of the die condition.

How a die is made

From profile drawing
to extrusion-ready die.

A clear technical handover reduces correction time. The process begins with the profile drawing and ends with feedback from the extrusion press.

01

Profile Analysis

Review the section drawing, circumscribed circle, wall thickness, alloy, press/container information and intended use. Establish whether the section requires a solid, hollow or semi-hollow die.

02

Die Design

Plan the die opening, bearing approach and supporting tooling. For hollow profiles, this includes the port, bridge, mandrel and welding-chamber arrangement.

03

CNC Machining

Machine the die and required components according to the approved drawing and tooling design. The work may include CNC milling, wire EDM, grinding and finishing operations.

04

Tool Preparation

Prepare the die and associated tooling for the customer’s production process. Any material, heat-treatment or surface-treatment requirement should be agreed before manufacture.

05

Die Correction & Polishing

Use trial output and press feedback to identify flow or dimensional issues. Bearing correction and related changes are made where required to improve the produced profile.

06

Inspection & Delivery

Confirm the agreed die and component dimensions, then prepare the tooling for dispatch. Keep the die reference and trial feedback available for any future correction or rework.

START WITH THE REQUIREMENT

Send the profile drawing, alloy, press/container size, billet size if available, and whether this is a new die or correction requirement.

Request a Quote
Profiles we support

Tooling for the
profile you need.

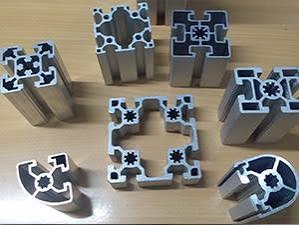
The end application changes the profile geometry. We work from the section drawing rather than assuming a standard die solution.

01

Architectural

Window, door, curtain-wall and façade sections. These often require multiple chambers, thin webs, drainage features and accurate visible surfaces.

02

Industrial

T-slots, machine frames, conveyors, guards, heat sinks and equipment sections. Die selection follows the section geometry and production requirement.

03

Electrical & Solar

Solar-module frames, LED housings, busbar covers, electrical enclosures and heat-dissipation profiles with repeatable section features.

04

Transport & Fabrication

Body-building, railings, ladders, partition systems and fabricated sections where profile dimensions must suit downstream cutting, machining and assembly.

05

Furniture & Interiors

Cabinet frames, partitions, trims, channels, handles and modular fittings made from open or hollow aluminium profiles.

06

Custom Profiles

A die is developed around your drawing, whether it is a one-off special section, an existing profile that needs a replacement die, or a revised version of a running profile.

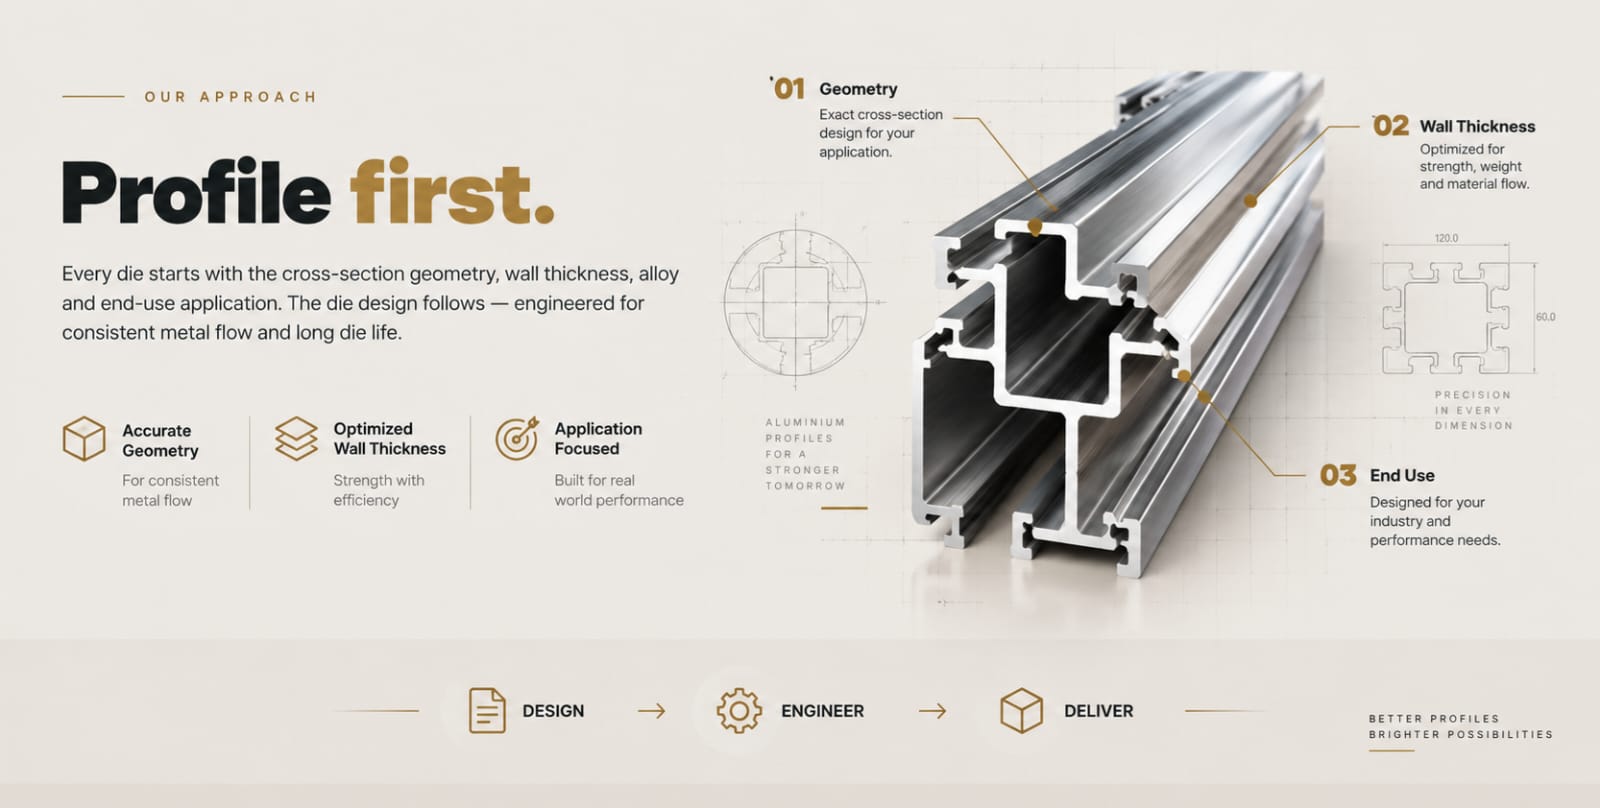
Our approach: profile-first aluminium extrusion engineering OUR APPROACH

Profile first.

Every die starts with the cross-section geometry, wall thickness, alloy and end-use application. The die design follows — engineered for consistent metal flow and long die life.

◇Accurate
Geometry
For consistent metal flow
▱Optimized
Wall Thickness
Strength with efficiency
◎Application
Focused
Built for real world performance
01 GeometryExact cross-section design for your application. 02 Wall ThicknessOptimized for strength, weight and material flow. 03 End UseDesigned for your industry and performance needs.
▤   DESIGN→⚙   ENGINEER→◇   DELIVER
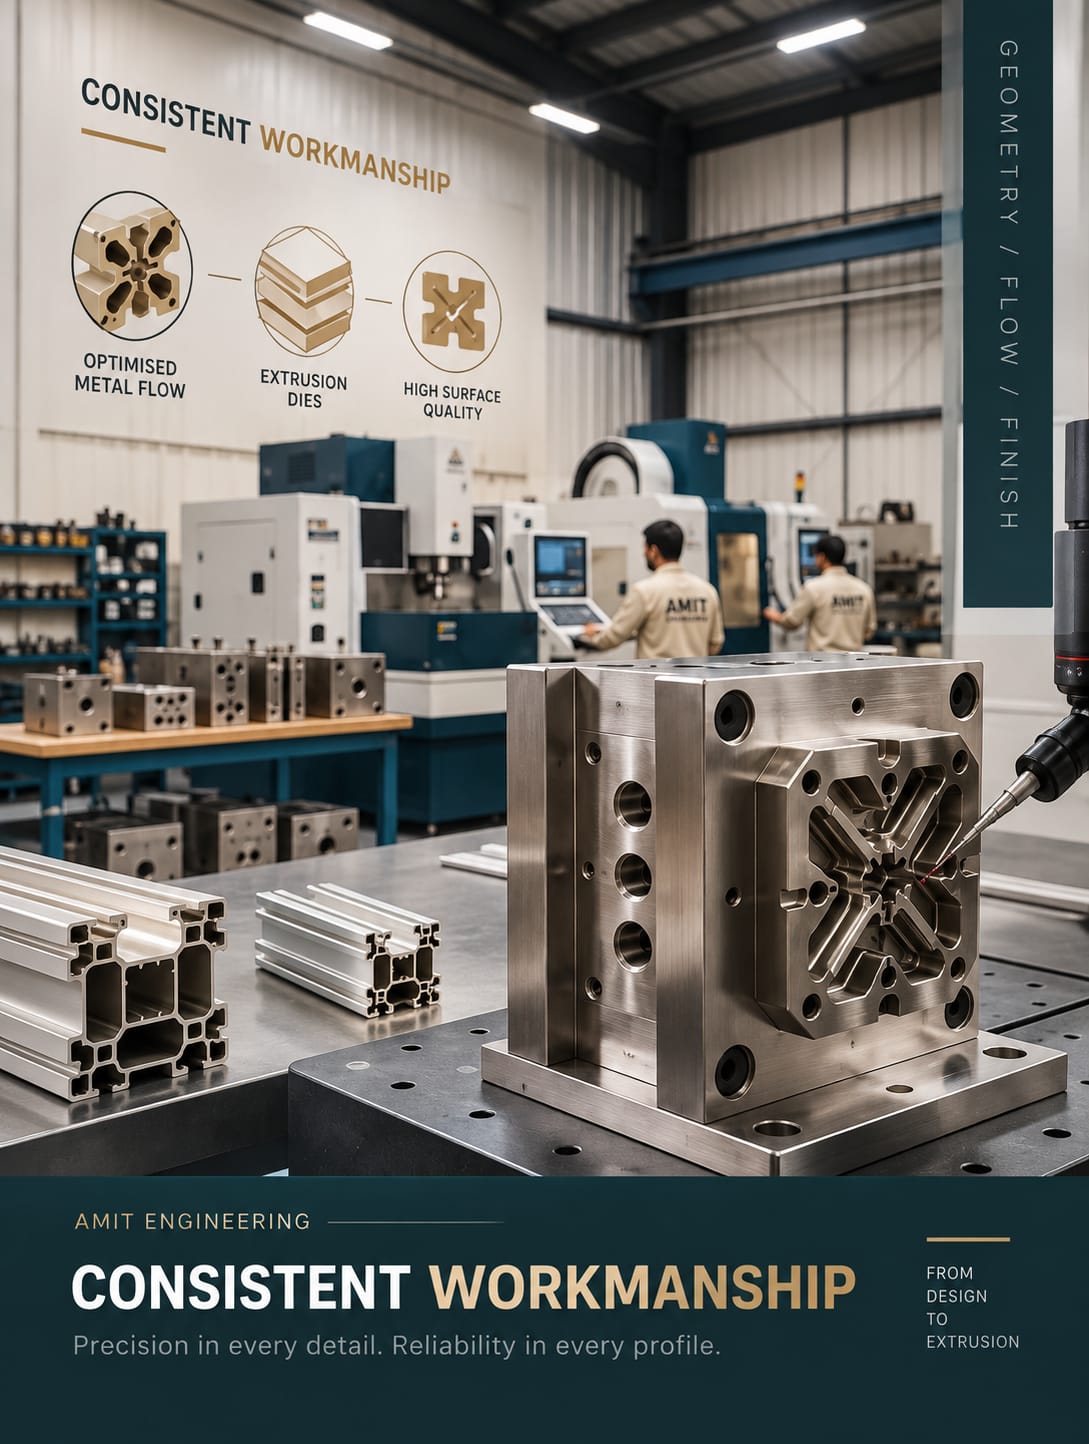
Quality

Consistent
workmanship.

The checks that matter depend on the profile and job scope. These are the key points to review before a die enters production.

GEOMETRY / FLOW / FINISH
Consistent workmanship and aluminium extrusion die quality
Why choose us

Precision. Speed.
Reliability.

A direct working relationship for new dies, running-profile corrections and replacement tooling.

Start with the actual profile.

For a useful die enquiry, send the section drawing and the production information you have. Existing die numbers, trial samples and press feedback are especially useful for correction jobs.

Request a Quote
Aluminium extrusion engineering visual
FROM DRAWING TO PRODUCTION
01 Profile Drawing→ 02 Die Design→ 03 Tool Manufacture→ 04 Trial & Correction
01

Profile-led review

The die solution is selected from the section geometry and extrusion requirement, not from a generic catalogue.

02

New dies & components

Die faces and supporting tooling for new profile development or replacement of production tooling.

03

Die Correction

Correction work based on what the press and profile sample show, including bearing-related adjustments where appropriate.

04

Ongoing Support

Keep die references and feedback on record to make repeat jobs, rework and replacement discussions clearer.

Contact

Send your
requirement.

Send the section drawing and available production details to Ankit Kushwaha, Managing Director. For correction work, include the existing die reference, profile sample and press feedback if available.

Get a quote / 01

Requirement details

Use this form to prepare an email enquiry. Attach your drawing manually in your email client before sending.

Drag & drop or click to upload

Your requirement has been saved. We will review the details and contact you shortly.